Your 12V power supply PCB layout passes DRC, but when you send the Gerbers out for a prototype quote, the fabricator flags a 0.12 mm gap near the controller. Can the factory hold that spacing with the 2 oz finished copper you specified? Moving one signal trace might clear the gap. Switching the whole layer to 1 oz copper also changes the resistance of the output path, so you’ll need to check voltage drop and temperature rise before approving it.
When you request a quote for a custom PCB fabrication service, ask for a DFM check against your actual stackup, finished copper weight and drill sizes. If you need a heavy copper PCB fabrication service, confirm which spacing and hole limits apply to the prototype and which will apply when you move to volume production. This guide walks through PCB design for manufacturability for a 12V power supply, from identifying the feature that triggered a fabrication query to choosing a fix and verifying its effect under load.
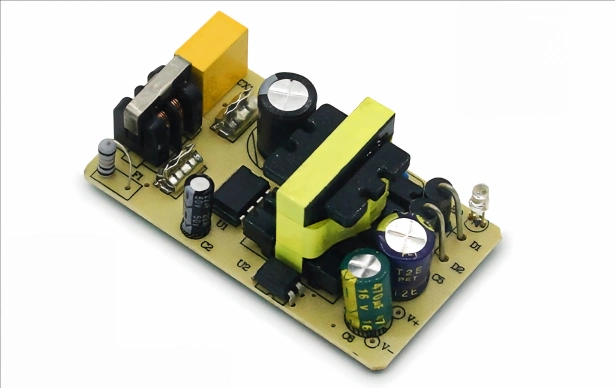
Align Design Specs with Your PCB Fabrication Service Capabilities
Before sending files for a turnkey PCB fabrication and assembly service, remember to set an engineering baseline between your CAD constraints and your manufacturer's standard process window.
- Define Exact Copper Weights and Tolerances: Specify both base copper and finished copper for each layer. Extract minimum trace width and spacing (W/S) from your Gerber files. For high-current traces, explicitly state the required minimum finished cross-sectional area or dimensional tolerances in your fabrication notes.
- Separate Drill Sizes from Finished Hole Sizes: Clearly distinguish mechanical drill bit diameter, finished hole diameter (FHS), minimum hole-wall copper thickness, and total finished board thickness.
- Distinguish Prototype vs. Volume Production Capabilities: Ask for the capability matrix matching your exact stackup. If the initial run is intended to validate a version for future mass production, evaluate it against mass-production standards. If it's only functional verification, you can use a prototyping process confirmed by the manufacturer, but make sure to record every feature that must be re-verified before volume release.
- Lock Down IPC Acceptance Standards: Specify the exact IPC-6012 revision and performance class (Class 2 vs. Class 3, depending on product requirement and failure consequences) on your procurement drawing. Reference IPC-A-600 for bare-board cosmetic acceptability and IPC-A-610 for final assembly electronics.2. Audit Three Core Power Supply PCB Parameters
Audit Three Core Power Supply PCB Parameters
When reviewing a 12V power supply PCB layout, focus first on copper weight, trace width/spacing, and via aspect ratios. The table below benchmarks typical heavy-copper capability data (referenced from KnownPCB capability guidelines) against common 12V power board design targets:
| DFM Parameter | Typical Fabricator Benchmark (KnownPCB Reference) | Common 12V Power Board Design Example | Red Flags Requiring Immediate Review |
|---|---|---|---|
| Copper Weight | Outer-layer compensation tables separate base copper from finished copper. | 1 oz base copper plated up to 2 oz finished copper on outer layers. | Order notes conflict with the stackup, or critical power layers omit finished copper weight. |
| Trace Width / Spacing (W/S) | For 1 oz base / 2 oz finished outer layers: 6/6 mil (prototype) and 7/7 mil (mass production). | Control/signal spacing at 0.12 mm (~4.7 mil); power pours sized independently for current and temperature rise. | Signal clearance falls below the copper-weight tier, or minimum etchable trace width is misused for power nets. |
| Hole Size / Annular Ring / Aspect Ratio | Mechanical drilling on heavy-copper boards typically supports up to an 8:1 aspect ratio; annular rings are verified per stackup. | 1.60 mm board thickness with a 0.20 mm drill bit (8:1 aspect ratio). | Confusing finished hole size with drill diameter, or shrinking holes without re-checking plating thickness and annular ring. |
Heavy copper etching results in undercut. Always verify the original Gerber features against your supplier's prototype or production W/S rules, and specify finished conductor requirements for primary current paths. Don’t treat CAM etch compensation as a 1:1 metric for single-sided copper loss, and never pre-compensate traces manually inside your Gerber files.
How Do You Fix DFM Issues in a 12V Power Supply PCB Layout?
Not every design that exceeds a manufacturer's standard capabilities needs a complete layout change. Based on the severity of the violation, modifications can be categorized into three tiers. This ensures manufacturability with minimal disruption to your power supply PCB performance.
Tier A: Localized Micro-Adjustments (No Architecture Change)
Use this when violations are isolated to specific traces, pads, or vias with adjacent routing room:
- Trace Width & Clearance Tweaks: If a 2 oz finished outer layer has two traces spaced at 0.12 mm against a 6 mil (0.1524 mm) prototype rule, nudge the traces apart by at least 0.032 mm and re-check neighboring clearances. If spacing violations occur between fixed IC footprint pads, review them against the component manufacturer's recommended land pattern.
- Annular Ring Expansion: Keep the drill size constant and increase the circular pad diameter by 0.10 mm to gain 0.05 mm of nominal annular ring per side—then verify that drill wander, layer-to-layer registration, and pad-to-pad clearances remain compliant.
- Via Stitching for Current Sharing: If a single via is overloaded, add parallel vias. Size the array based on total current, layer-transition length, minimum barrel copper, and copper pour entry/exit width.In asymmetrical layouts, the current distribution among individual vias may vary.
Tier B: Rule & Stackup Re-Optimization
Use this when local nudging cannot resolve conflicts between high-current pours and fine-pitch control ICs:
- Selective Layer Copper Weight: Instead of running heavy copper across all layers, compare assigning heavier copper only to dedicated power layers, widening primary power polygons, or reassigning signal layers. Note that selective thickness within a single layer requires special process approval and cost review from your custom PCB fabrication service.
- Step Up W/S Rules with Copper Weight: Tighter copper requires wider spacing. For example, moving from 2 oz finished (6/6 mil proto, 7/7 mil volume) to 3 oz finished (2 oz base) shifts standard outer-layer limits to 8/8 mil (proto) and 9/9 mil (volume). After widening clearances, re-verify the trace widths, pay particular attention to the routing segments connected to fine-pitch controller pins.
- Reduce Via Aspect Ratio: Lower aspect ratios by increasing drill diameter or reducing board thickness. For example, with a drill depth of 1.60mm, a 0.20mm drill bit means an 8:1 aspect ratio, whereas a 0.16mm drill pushes it to 10:1. Adding parallel vias can lower current per via, but the aspect ratio of each individual via is still determined by its own depth and diameter. If a PCB manufacturer quotes based on finished hole sizes, make sure all hole diameter specifications are calculated on a consistent basis.
Tier C: Qualify a Specialized PCB Fabricator
If your current PCB manufacturer cannot simultaneously meet your requirements for finished copper weight, fine-pitch spacing, and barrel plating specs, and modifying the layout would compromise electrical performance, you may submit the identical fabrication package to a specialized heavy copper PCB fabrication service or ISO certified PCB fabrication service. For instance, 4 oz finished outer copper (3 oz base) typically requires 10/10 mil (proto) and 12/12 mil (volume) rules. Confirm in writing that the supplier can reliably build your exact worst-case trace/drill combination—not just the copper weight in isolation.
Re-Verify Current Capacity and Thermal Paths After DFM Edits
Every physical layout change alters electrical resistance or heat dissipation. Before locking your PCB design for manufacturability changes, trace both paths from input to output:
- Recalculate Voltage Drop & Conductor Temperature Rise: Reference IPC-2152 using actual load current, cross-sectional area, and allowable temperature rise. Assuming length, width, and ambient temperature constant, dropping finished copper from 2 oz to 1 oz, the DC resistance of that segment will roughly double, as will the I²R power loss and voltage drop. Avoid generic internal-vs.-external layer derating rules; evaluate actual heat sinking.
- Audit the Complete Thermal Path: Heat travels from switching FETs and inductors through pads, copper planes, and thermal via arrays to opposite-side copper or chassis heatsinks. Finished hole diameter, barrel copper thickness, effective thermal length, and via pitch all influence thermal resistance. Validate hotspot temperatures via thermal simulation or first-article bench testing.
- Evaluate Solder-Mask Windows Carefully: Leaving solder mask off high-current traces to add solder during assembly does not increase underlying copper cross-section. Before using exposed tinning for thermal relief, confirm with your turnkey PCB fabrication and assembly service that they can control solder thickness and prevent solder bridging to adjacent pads, then verify actual temperature reduction under the same load and enviromental conditions.
- Define First-Article Bench Acceptance Metrics: Measure full-load voltage drop from the output capacitor positive terminal to the output connector positive terminal under specified ambient temperature and airflow. Log hotspot temperatures at narrow copper necks and thermal via arrays against your design limits.
What should you send with your prototype RFQ?
To eliminate revision mix-ups or missed process callouts when submitting to a mass production PCB fabrication service, lock down four deliverables:
- DFM Decision Matrix: Maintain a single sign-off sheet logging Original Design Value vs. Fabricator Capability vs. Pass/Fail Status vs. Final Modification vs. Current/Thermal Impact.
- Version-Controlled Manufacturing Archive: Bundle final Gerbers, stackup and finished copper drawings, NC drill files (explicitly separating plated vs. non-plated holes), and special process notes (via plugging, solder mask dams, impedance tolerances) under one unique revision ID.
- Final Pre-Production DFM Sign-Off: Have your fabricator run a final CAM/DFM check on the frozen files and confirm in writing that all heavy-copper, drill, and IPC class requirements are accurately captured.
- First-Article Test Baseline: Attach your planned voltage-drop and thermal test checklist to the prototype traveler so the exact same pass/fail criteria carry seamlessly into volume production.
Technical references
[1] KnownPCB — Outer-layer heavy copper design rules
[2] KnownPCB — PCB fabrication capabilities by product type
[3] KnownPCB — High-current PCB via design
[4] IPC-6012F — Qualification and Performance Specification for Rigid Printed Boards
[5] IPC-A-610J — Acceptability of Electronic Assemblies
[6] IPC-2152 — Standard for Determining Current Carrying Capacity in Printed Board Design